The purpose of the Journal is to build-up and share our knowledge in manufacturing as a contribution toward the high-tech manufacturing movement in Armenia.
Published by the Engineering Association
The EC Manufacturing JournalIssue 2/2026Published by the Engineering AssociationYerevan, June 15, 2026
An interesting article that combines technology, science, art, history, skills, philosophy, observations, analysis, experimentation, discoveries, and suggestions how to move forward. The article is written in an easy and intriguing style for professionals and non-professionals alike.
From Renaissance Masterpieces to Titanium Turbines: How a 5-Axis CNC Machine Works
by Armen Arustamyan, YEA Manufacturing
English translation
Hello everyone! My name is Armen Arustamyan, I am a mechanical engineer and I am responsible for mechanical production at YEA Engineering.
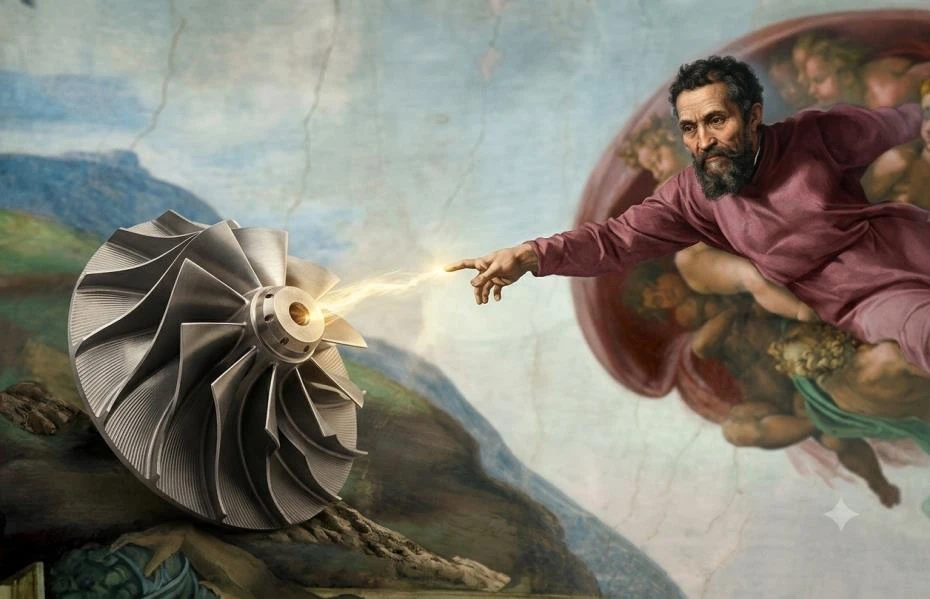
There is a popular tale that when Michelangelo was asked how he created his sculptures, he replied: “I simply take a block of marble and cut away everything superfluous.” It sounds beautiful, of course. But I would like to see how he would “simply cut away everything superfluous” from a solid blank of a complex aerospace part.
In production, every day we make parts that a few decades ago would have been considered practically impossible. So today, without any fluff, I want to talk about what I work with myself — 5-axis milling machines. Let’s try to break this technology down in plain human language, so that it is clear how it really works and why it is so cool.
What is 5-axis machining and why is it needed?
• To put it very simply, 5-axis machining is when the machine can move the cutting tool or the part along five axes simultaneously. That is exactly why such machining is widely used in the aerospace industry and in making complex parts such as impellers. Why do we in production love this technology so much? It’s simple:
• The “done in one setup” principle. You load the blank, clamp it — and the machine machines it from practically all sides. There is no need to take the part out, flip it, make complex fixtures and re-set the zeros. This saves a lot of time and reduces errors associated with re-clamping.
• Hard-to-reach areas can be machined. The machine tilts the part or the spindle so that we can mill complex geometry (for example, undercuts) while avoiding collisions between the tool and the part or the table. The tool lasts longer because it always works at the correct angle to the metal. Cutting is smoother, the machine does not chatter, and the surface quality improves.
What do René Descartes, a fly and airplanes have to do with it?
To understand where these 5 axes come from, let’s remember school. Everyone knows the story of Newton and the apple, but there is a similar tale about the philosopher and mathematician René Descartes.
Once Descartes was lying in bed (philosophers generally loved doing that) and watching a fly circling the room. And then he realized that the exact position of this fly in space could be described with just three numbers: length, width and height.
That is how the Cartesian coordinate system appeared — X, Y and Z. On a machine these are the basic movements: left-right, forward-back and up-down. These are the classic three axes.
But where do the other two come from?
Now imagine that fly in flight in close-up. It doesn’t just move as a point in space — it also changes its orientation.
Here it is convenient to compare the machine’s axes with the movements of an airplane:
Imagine the airplane banking onto a wing. This is rotation about the longitudinal X axis. In CNC this is usually called the A axis.
When the airplane raises or lowers its nose (pitch), this is rotation about the Y axis. In machines this is the B axis.
And when the airplane turns its nose left or right parallel to the ground (yaw), this is rotation about the vertical Z axis. In machines this is the C axis.
A full 5-axis machine uses the classic X, Y, Z movements and adds two rotary axes to them (for example, rotating the table about the C axis and tilting about the A axis). That’s all the “magic”.
The A, B and C axes are usually designated in alphabetical order, corresponding to the rotary movements about the X, Y and Z axes. Although 6-axis CNC machines also exist, 5-axis configurations are more common, since in most cases the sixth axis does not give a significant practical advantage.
A final note on the notation: in a vertical machining center the X and Y axes lie in the horizontal plane and the Z axis is vertical. In a horizontal machining center the axis orientation is different: the Z axis remains vertical, while the arrangement of the X and Y axes depends on the specific machine layout.
So how many axes do you actually need?
Sometimes in equipment catalogs or at exhibitions you can come across “monsters” claiming 7, 9 or even 11 axes. It sounds out of this world. It seems that programming such a machine would require a team of NASA scientists. But in fact everything is much simpler than it seems.
As Mike Finn, one of the leading engineers at Mazak America, rightly explains, a large number of axes appears not because the part goes into some fourth dimension. It is all about the number of “working units” inside a single machine.
Imagine a fancy multi-function machine. It may have not one spindle but two (a main spindle and a sub-spindle), plus two turrets — an upper and a lower one. The upper turret moves along its own axes, the lower one along its own, and the sub-spindle adds yet another degree of freedom.
In total this can give 9 or more axes in a single machine. In essence, such a machine works like a Swiss army knife: it can turn, mill and perform operations in parallel, without re-clamping the part.
But here it is important to understand one key engineering idea that is often voiced in the industry: however many axes the machine itself has, the geometry of the part remains five-axis.
Take, for example, a complex aircraft valve or an impeller. We can machine it on an ordinary 5-axis vertical machine. Or we can use a multi-axis machining center with a tilting B axis, two spindles (two C axes), the standard X, Y, Z movements, and an additional lower turret with its own X and Z axes.
There are many axes, the machine looks like a Transformer inside, but the finished part itself remains the same five-coordinate part in terms of its geometry.
All these “additional” axes are needed not to complicate the shape but to increase productivity: to perform more operations in one cycle, to combine turning and milling, and not to waste time on re-clamping the part and on extra steps.
The brain of the machine: an overview of CAM systems and my personal choice
When it comes to five axes, writing a program by hand is almost science fiction. Trying to calculate in your head a toolpath in which five axes move and rotate simultaneously is the fastest way to get confused and send an expensive spindle for early repair. Without CAM systems an engineer here is helpless.
The software market is huge, but every popular solution has its own peculiarities, which I would summarize as follows
Autodesk Fusion 360: an excellent tool for getting started or for simple positioning. But when it comes to heavy multi-axis machining, its basic capabilities begin to fall short, and buying additional Extensions does not always meet expectations because of the difficulty of fine-tuning post-processors.
SolidCAM: the integration with SolidWorks is convenient, and the proprietary iMachining roughing strategy really performs well. However, its spindle collision-control algorithms in complex five-axis machining are inferior to specialized higher-end solutions.
Siemens NX: a true industrial giant. In it you can build a toolpath for a part of practically any complexity, but the interface demands something like separate training and a great deal of patience from the engineer. The entry threshold here is extremely high.
What I chose for our production and why
Having analyzed these solutions, for continuous 5-axis machining at YEA Engineering I bet on the combination of HyperMILL and VERICUT.
HyperMILL (from Open Mind) is perhaps one of the best solutions for simultaneous five-axis machining. Its toolpath algorithms for turbine blades, channels and impellers work very stably. The program itself determines at what angle to tilt the tool in order to remove material efficiently and avoid the fixtures.
But however “smart” a CAM system may be, it works within its own mathematical models. It does not see exactly what will come out after the post-processor in the final G-code.
That is why I paired hyperMILL with VERICUT. It is an independent digital twin of the machine. It takes the “raw” G-code that will go to the controller and simulates the machining as close to reality as possible. VERICUT makes it possible to detect axis over-travel, errors in the code and potential collisions.
The combination of hyperMILL (as the toolpath generator) and VERICUT (as the independent checker) is my personal insurance against crashes on equipment whose cost is measured in hundreds of thousands of dollars.
At the same time, for positional machining in “3+2” mode I kept Mastercam. It has intuitive work with planes, and its high-speed 2D and 3D milling algorithms (Dynamic Milling) are still considered among the best. When simultaneous rotation of the axes is not needed, Mastercam makes it possible to prepare NC programs faster and more simply than heavier multi-axis systems.
Understanding the terms: what “3+2” is and how it differs from true 5-axis
There is often confusion in professional circles: if a machine has five axes, any machining on it is called five-axis. In fact these are two fundamentally different processes.
“3+2” mode (positional machining)
Imagine a part that needs to be machined from all sides. In order not to re-clamp it by hand (and not to lose datum accuracy), the machine’s two rotary axes turn the blank to the required angle relative to the spindle.
Once the part has taken the required position, the rotary axes are locked. The machine effectively turns into a rigid 3-axis center and works along the X, Y and Z axes.
Then the logic is simple: machine one side, stop, unlock the rotary axes, turn the part to a new position, lock again and continue machining.
In this mode the rotary axes take part only in positioning between passes, and the cutting itself proceeds as in ordinary 3-axis machining. This is exactly the kind of task Mastercam is suited for: fast toolpath generation and stable work in “3+2” mode.
Continuous 5-axis machining — the arena of hyperMILL
Here everything works differently. The machine does not stop anywhere and does not lock anything. All five axes move simultaneously in real time.
Why is this needed? Imagine a curved impeller blade. Its surface must be as smooth as possible. If the tool stops or the toolpath is interrupted (as in “3+2” mode when moving between positions), a step or a transition mark may appear on the surface. For aerodynamic parts this is already a potential defect.
That is why the cutter must traverse the entire complex surface in one continuous pass, smoothly following its shape. The tool constantly changes position and tilt right during cutting, without stops or jerks. It is for such tasks that I chose hyperMILL — its mathematical algorithms handle continuous five-axis toolpaths well, enabling stable machining of complex geometry with high surface quality.
Finale: equipment, reality and a little philosophy
Our flagship for all this complex geometry is the HAAS UMC-750SS five-axis machining center.
One of the most telling parts we have made on it is an impeller. Looking at such a part, you immediately understand why five axes are needed at all.
But let’s take off the rose-tinted glasses: full continuous five-axis machining is not used in 90% of everyday orders. And that is absolutely normal — that is how the market works all over the world. Such technologies are in demand primarily in aviation, space and high-tech manufacturing.
Then why invest in five axes if 90% of the work is three? It’s simple: I clearly understand where technology is heading. Almost every month new machining strategies, new tools and software solutions appear that change the rules of the game. Staying on the sidelines means gradually falling behind.
And finally — back to where I started. Modern CAM software is just a tool, like Michelangelo’s hammer and chisel. But what the result will be — just a machined blank or a truly complex, high-quality part — depends on the engineer at the machine.
That is why, in addition to hard technical skills, spatial thinking matters in our work, along with a bit of the approach of a designer and an artist at the same time.
That’s all. I am Armen Arustamyan, and if after this article you finally have a picture of how a five-axis machine works, then we did not waste our time. See you.